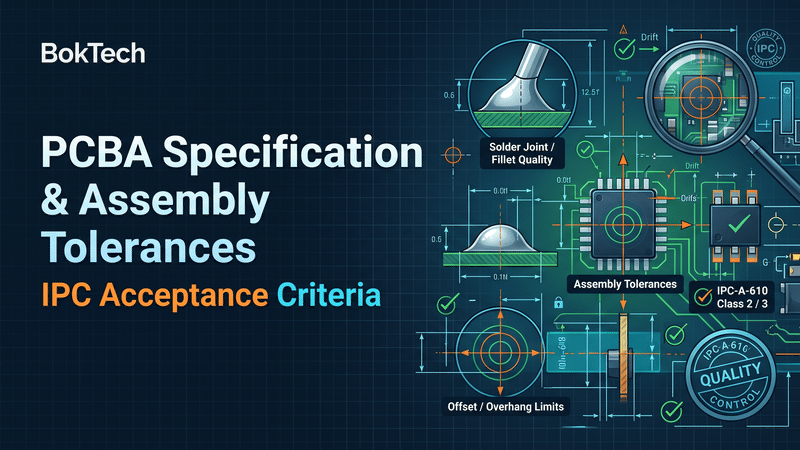
Quick Takeaway (TL;DR): While a bare-board fabrication specification defines how raw laminate is etched and plated, a PCBA Assembly Specification establishes the legal and technical criteria for component placement, metallurgical solder joint formation, and functional verification. Without an explicit assembly specification, "acceptable workmanship" remains completely subjective. Engineering sign-off must reference recognized industrial standards—specifically IPC-A-610 Class 2 (Dedicated Service Electronic Products) or IPC-A-610 Class 3 (High-Performance / Harsh-Environment Electronics). A production-ready assembly specification explicitly defines X/Y/theta placement tolerances, minimum heel/side/toe solder fillets, BGA/QFN thermal pad voiding limits (< 15% to 25%), mandatory inspection stages (3D SPI, 3D AOI, 3D AXI), and First-Article Inspection (FAI) acceptance criteria before production lines are scheduled.
1. The Dual Specification Framework: Fabrication vs. Assembly
A common engineering failure during new product introduction (NPI) is treating the bare board and the assembled board as a single manufacturing step.
Bare-board fabrication and surface-mount assembly operate under completely different physical constraints, chemical processes, and quality standards:
| Engineering Parameter | Bare-Board Fabrication Specification | PCBA Assembly Specification |
| Governing Standard | IPC-6012 (Rigid) / IPC-6013 (Flex-Rigid) | IPC-A-610 (Acceptability of Electronic Assemblies) / J-STD-001 |
| Physical Scope | Copper traces, dielectric cores, hole plating, soldermask | Solder paste deposition, component placement, solder joint integrity |
| Primary Tolerances | Finished board thickness (±10%), drill diameter (±0.05mm) | Component X/Y offset, rotational skew, coplanarity, lead overhang |
| Defect Classifications | Annular ring breakout, etch undercut, delamination | Solder bridging, voiding, tombstoning, Head-in-Pillow (HiP), opens |
| Primary Test Method | Flying probe netlist continuity & isolation test | 3D SPI, 3D AOI, 3D AXI X-ray, In-Circuit Test (ICT), Functional Test (FCT) |
Review our PCB manufacturing files guide to verify the data package required before applying assembly specifications, and explore our low-volume PCB assembly services for prototype handoff workflows.
2. Component Placement Tolerances: SMT Offset and Rotational Skew
Component placement tolerance defines how far a part may deviate from its theoretical centroid coordinates (X, Y, and rotation angle theta) and still achieve acceptable wetting during reflow soldering.
Pre-Reflow Placement vs. Post-Reflow Self-Alignment
Surface mount pick-and-place systems operate with mechanical placement accuracies of ±25 µm to ±50 µm at 3-sigma. During reflow soldering, the surface tension of molten solder naturally pulls two-terminal passives and symmetrical ICs toward pad centers (self-alignment).
However, a specification must never rely entirely on self-alignment:
•Parts placed with excessive pre-reflow offset (> 25% of pad width) experience asymmetrical wetting forces, resulting in tombstoning (part standing on end) or rotational skew.
•Multi-pin fine-pitch packages (QFP, SOIC) and connectors do not self-align; rotational errors translate into severe pin-to-pad overhang on corner leads.
| Component Package Family | Max Pre-Reflow X/Y Offset | Max Post-Reflow Side Overhang (A) | Max Post-Reflow End Overhang (B) | Max Allowable Rotational Skew (Theta) |
| Discrete Passives (0402 / 0603) | ± 0.05mm (± 2.0 mil) | ≤ 25% of component termination width | No overhang permitted inside pad | ± 3.0° maximum angular deviation |
| Ultra-Small Passives (0201 / 01005) | ± 0.025mm (± 1.0 mil) | ≤ 15% of component termination width | No overhang permitted inside pad | ± 1.5° maximum angular deviation |
| Gull-Wing ICs (QFP / SOIC) | ± 0.035mm (± 1.4 mil) | ≤ 25% of lead width (Class 2) / ≤ 15% (Class 3) | Solder fillet must wet toe and heel | ± 0.5° maximum angular deviation |
| Bottom-Terminated (QFN / DFN) | ± 0.030mm (± 1.2 mil) | ≤ 25% of lead width (Class 2) / ≤ 15% (Class 3) | Lead must not overhang outside pad | ± 0.5° maximum angular deviation |
| Fine-Pitch BGA (≤ 0.50mm pitch) | ± 0.025mm (± 1.0 mil) | Solder ball must wet 100% of pad surface | Fully centered within solder mask | ± 0.25° maximum angular deviation |
| Through-Hole Connectors (THT) | ± 0.075mm (± 3.0 mil) | Pin centered in plated through-hole barrel | Lead protrusion: 0.5mm to 1.5mm | ± 1.0° maximum angular deviation |
3. Solder Joint Acceptance Criteria: IPC-A-610 Class 2 vs. Class 3
Referencing IPC-A-610 establishes clear, objective visual and metallurgical acceptance standards. Specifying the target class (Class 2 vs. Class 3) directly affects production yields, inspection rigor, and final assembly costs.
•IPC-A-610 Class 2 (Dedicated Service Electronic Products): Covers commercial computing, communication equipment, industrial controls, and consumer electronics where continuous operation is desired but uninterrupted service is not critical.
•IPC-A-610 Class 3 (High-Performance / Harsh-Environment Electronic Products): Mandatory for aerospace, medical life support, automotive safety systems, and mission-critical server hardware where equipment downtime cannot be tolerated.
| Solder Joint Feature | IPC-A-610 Class 2 Standard | IPC-A-610 Class 3 Standard | Primary Mechanical & Electrical Failure |
| Gull-Wing Heel Fillet Height (F) | Minimum 50% of lead thickness (T) | Minimum 75% of lead thickness (T) | Joint fatigue cracking under thermal cycling |
| Gull-Wing Side Fillet Extension | Wetting visible along lead side | Wetting extends ≥ 3× lead width or 0.5mm | Lead lifting under mechanical vibration |
| QFN End Fillet (Toe) Wetting | Not required unless specified on drawing | Mandatory toe fillet if pad extension exists | Lower mechanical shear strength |
| Through-Hole Barrel Fill | Minimum 75% vertical solder fill | Minimum 100% vertical solder fill (360°) | Pin detachment under mechanical tensile stress |
| Solder Wetting Angle (θ) | Contact angle θ ≤ 90° | Contact angle θ ≤ 90° (Well-feathered edge) | Cold solder joint or dewetting |
| Cleanliness / Flux Residue | Visual clean; no sticky active residue | Strict ionic contamination < 1.56 µg/cm² NaCl | Dendrite growth and electrochemical migration |
4. Area-Array (BGA/QFN) and Thermal Pad Voiding Limits
Because Area-Array packages (BGA, WLCSP, LGA) and bottom-terminated components (QFN, DFN, PowerPAK) have hidden solder connections, visual inspection is impossible. The assembly specification must establish strict X-ray radiographic inspection thresholds.
Solder Joint Voiding Thresholds
Solder voids form during reflow when flux volatiles outgas and become trapped inside the molten solder pool.
•IPC-7095 Standard for BGA Balls: Total voiding area within any individual BGA ball must not exceed 25% of the total ball radiographic projection area (Class 2). For high-reliability Class 3 assemblies, voiding must remain below 15%.
•QFN Thermal Ground Slugs: High-power processors and motor drivers dissipate heat into internal PCB copper planes through bottom thermal pads. The assembly specification must establish a maximum voiding limit of 15% to 20% (uncontrolled reflow profiles regularly exhibit 35% to 50% voiding, causing silicon thermal throttling).
| Package & Joint Type | Standard IPC Class 2 Void Limit | High-Reliability Class 3 Void Limit | Inspection Technique Required |
| BGA Solder Balls (Signal) | ≤ 25% of ball image area | ≤ 15% of ball image area (No single void > 8%) | 3D Automated X-ray Inspection (AXI) |
| BGA Solder Balls (Corner Pins) | ≤ 20% of ball image area | ≤ 10% of ball image area | 3D AXI (Checks high-strain corners) |
| QFN Thermal Ground Pad | ≤ 25% to 30% total voiding | ≤ 15% total voiding | 2D / 3D X-Ray Inspection |
| Power Discrete (D2PAK / DFN) | ≤ 20% total voiding | ≤ 10% total voiding | 2D / 3D X-Ray Inspection |
| Through-Hole Solder Fillet | Solder voids ≤ 30% of barrel volume | Solder voids ≤ 20% of barrel volume | Micro-section coupon or X-ray |
Radiographic Defect Callouts
The assembly specification must classify the following area-array conditions as immediate non-conformances:
1. Head-in-Pillow (HiP): A defective joint where the BGA ball coalesces with itself and rests against the solder paste deposit on the board without metallurgical bonding.
2. Solder Ball Bridging: Solder short-circuits between adjacent balls (pitch ≤ 0.50mm).
3. Non-Wet Opens: Incomplete reflow where the solder ball fails to wet the PCB pad land pattern.
4. Solder Splatter / Extruded Balls: Solder micro-beads ejected outside the component perimeter exceeding 0.10mm diameter.
5. Multi-Stage Inspection Architecture: Detection Capabilities
Relying on a single final visual inspection or basic post-reflow Automated Optical Inspection (AOI) guarantees that latent soldering defects will escape into customer shipments.
A production assembly specification must designate specific quality verification gates:
| Quality Inspection Gate | Detection Mechanism & Technology | Critical Manufacturing Defects Caught | Production Phase Implemented |
| 1. 3D Solder Paste Inspection (SPI) | Laser triangulation & structured light | Paste volume (too high/low), height, area, offset, bridging | Immediately post stencil printing |
| 2. Pre-Reflow Optical Inspection | High-resolution machine vision cameras | Missing parts, rotated ICs, polarity reversal, gross offset | Between pick-and-place and reflow oven |
| 3. Post-Reflow 3D AOI | Multi-angle cameras + laser height profiling | Solder bridges, tombstones, lifted leads, dry joints | Immediately post reflow cooling |
| 4. 3D Automated X-Ray (AXI) | High-voltage transmission X-ray tube | BGA voiding, Head-in-Pillow, hidden shorts under QFNs | Post reflow on sample or 100% basis |
| 5. In-Circuit Testing (ICT) | Bed-of-nails contact pin fixture | Resistor/capacitor values, net continuity, open traces | Post SMT/THT assembly prior to casing |
| 6. Flying Probe Testing (FPT) | Automated high-speed moving test needles | Component values, diode drops, shorts (No tooling needed) | Low-volume prototype verification |
| 7. Functional Testing (FCT) | Custom test harness, power rails, firmware | Operational bus communication, RF power, LED status | Final acceptance prior to box packaging |
Explore our complete equipment and inspection capabilities to review the verification systems active on our production floors.
6. Special Package Handling, MSL, and Hardware Assembly Notes
Specialized electronic components require environmental and mechanical handling controls that must be formally documented in the assembly specification notes:
Moisture-Sensitive Devices (MSD / J-STD-020)
Semiconductor packages absorb atmospheric moisture. When passed through lead-free reflow ovens (240°C–260°C), internal moisture instantly vaporizes into steam, causing internal silicon delamination or external package rupturing (the "popcorn" effect).
•Specification Rule: Mandate that all components rated MSL 3, MSL 4, MSL 5, or MSL 5a must be baked per J-STD-033 standards (typically 125°C for 24 to 48 hours) if exposure time exceeds floor life limits.
•Packaging: Components must remain sealed in Moisture Barrier Bags (MBB) with desiccant and Humidity Indicator Cards (HIC) until immediately prior to feeder loading.
Press-Fit Connector Installation
Press-fit connectors rely on compliant mechanical pins driven into finished plated through-holes without solder.
•Specification Rule: State the required insertion tool fixture, press speed, and maximum allowable seating force per pin (typically 20N to 40N).
•Inspection Criteria: Verify zero pin deformation, proper pin shoulder seating against the PCB surface, and lead protrusion compliance.
Conformal Coating Requirements
If the board operates in humid, dusty, or outdoor marine environments, specify conformal coating parameters:
•Coating Material: Acrylic (AR), Polyurethane (UR), Silicone (SR), or Parylene (XY) per IPC-CC-830.
•Coating Thickness: Typically 25 µm to 75 µm (1.0 to 3.0 mils) dry film thickness.
•Keep-Out Zones: Explicitly document masking zones for connectors, test points, RF shielding can boundaries, and pushbuttons on the assembly drawing.
7. Electrical Testing, First-Article Inspection (FAI), and Traceability
To bridge the gap between mechanical assembly and functional reliability, define documentation and traceability deliverables:
First-Article Inspection (FAI) Protocol
Before authorizing volume production, the assembly facility must produce and document a comprehensive First Article:
1. AS9102 / IPC FAI Report: Complete verification matching every component placement, polarity, and value against the master BOM.
2. Solder Joint Radiographic Report: 3D X-ray images validating BGA ball wetting, thermal slug voiding, and lead alignment.
3. Reflow Thermal Profiling Chart: Actual temperature recording from a multi-channel thermocouple datalogger verifying soak time, Time Above Liquidus (TAL: 60–90 seconds @ >217°C for SAC305), and peak temperature (238°C–245°C).
Traceability and Device Serialization
For medical, automotive, and high-reliability industrial hardware, specify the depth of production lot tracking:
•Level 1 (Batch Traceability): Solder paste lot number, reflow oven line ID, and assembly date code.
•Level 2 (Unit Traceability): Unique 2D DataMatrix barcode laser-marked onto each PCB linking individual boards to SMT placement logs, SPI/AOI image archives, and functional test logs.
•Level 3 (Component Traceability): Full traceability mapping specific silicon reel lot codes to individual board serial numbers.
For comprehensive bare-board fabrication parameters, consult our PCB fabrication specification guide and our PCB assembly services overview.
8. The Master PCBA Specification Checklist
Compile your assembly specification drawing using this checklist to eliminate manufacturing ambiguities:
| Specification Section | Mandatory Parameter to Document | Engineering Acceptance Threshold | Manufacturing Risk If Omitted |
| 1. Workmanship Standard | IPC-A-610 Class 2 or Class 3 callout | Class 2 for commercial; Class 3 for mission-critical | Unenforceable inspection standard; scrap disputes |
| 2. Placement Tolerances | Max allowable X/Y offset and angular skew | Package-specific (e.g., ≤ 25% lead width overhang) | Tombstoning, pin bridging, connector misalignment |
| 3. Solder Alloy Chemistry | Solder alloy composition and flux type | SAC305 (Sn96.5/Ag3.0/Cu0.5) Lead-Free / ROL0 Flux | Incompatible reflow thermal profile; weak joints |
| 4. BGA & QFN Voiding | Maximum radiographic void percentage | Signal balls < 15%; QFN thermal pad < 20% | Silicon thermal throttling and joint fatigue failure |
| 5. Inspection Stages | Required verification gates | 100% 3D SPI + 100% 3D AOI + 3D AXI for BGAs | Hidden solder opens escaping to customer assembly |
| 6. MSL Handling | Baking and moisture control per J-STD-033 | Floor life tracking on MSL 3+ active silicon | Package delamination ("popcorning") during reflow |
| 7. First-Article Review | FAI documentation and customer sign-off | Signed FAI report + X-ray image archive | Batch manufacturing errors across full production run |
| 8. Testing Scope | In-Circuit Test (ICT) / Functional Test (FCT) | Written functional test procedure & cycle times | Electrically non-functional boards shipped in volume |
9. Frequently Asked Questions (FAQ)
What is the maximum allowable solder voiding percentage for BGA balls under IPC-A-610?
Under IPC-A-610 and IPC-7095, the standard acceptance threshold for BGA solder balls is less than 25% of the total ball area when viewed by 2D/3D X-ray. However, for high-reliability automotive and compute systems operating under IPC Class 3, engineering specifications routinely enforce a tighter threshold of less than 15% total voiding, with no single void exceeding 8% of the ball area.
When should a hardware engineering team mandate IPC-A-610 Class 3 over Class 2?
Mandate IPC Class 3 whenever the end product operates in harsh environments (extreme temperature swings from -40°C to +125°C, high mechanical vibration, or continuous 24/7 mission-critical uptime), such as aerospace, medical implants, automotive ADAS controllers, or data-center AI accelerator cards. Consumer electronics, standard IoT devices, and non-critical commercial products are appropriately governed by Class 2.
Can post-reflow Automated Optical Inspection (AOI) replace 3D Solder Paste Inspection (SPI)?
No. Over 70% of all surface-mount soldering defects (including bridging, tombstoning, voiding, and insufficient wetting) originate during the solder paste printing process. 3D SPI detects insufficient paste volume, pad bridging, and stencil misalignment before components are placed, allowing boards to be cleaned and reprinted. Post-reflow AOI can only detect defects after the permanent metallurgical joint has formed, forcing expensive manual rework.
How should component polarity be documented to prevent reversed SMT placement?
Component polarity must never be inferred from CAD library footprint shapes alone. Polarity must be explicitly documented on the Assembly Drawing (PDF) using bold, unambiguous markers: a prominent dot for Pin 1 on all ICs, clear "+" symbols for tantalum/electrolytic capacitors, and distinct diode cathode bar markings. Stating "Centroid file generated per IPC-7351 0° orientation conventions" in your assembly notes ensures pick-and-place rotation alignment.
10. From Prototype to Full-Scale PCBA Production: Partner with BokTech
Transforming an advanced hardware design into a defect-free, volume-manufactured electronic product requires close alignment between engineering specifications and factory-floor assembly processes:
•Achieving high assembly yields across 0.35mm–0.50mm micro-BGAs, WLCSP, and 01005 passives without bridging or voiding.
•Enforcing strict IPC-A-610 Class 2 and Class 3 solder joint standards with 100% 3D SPI and high-resolution 3D AXI verification.
•Validating automated functional testing (FCT) and firmware programming protocols to ensure 100% electrical compliance.
•Sourcing authentic, fully traceable components directly through authorized global distribution networks.
BokTech delivers end-to-end turnkey PCB manufacturing, high-precision SMT assembly, and complete box-build integration operating directly from our advanced facility in Shenzhen. We provide:
•Complete Bare-Board to PCBA Integration: 1 to 32 layer multi-layer fabrication, Any-Layer HDI, heavy copper power planes (up to 5 oz), and precision SMT placement under one roof.
•Certified Quality Standards: 100% adherence to IPC-A-610 Class 2 and Class 3 workmanship, ISO 9001, ISO 13485 (Medical), and IATF 16949 (Automotive) quality management systems.
•High-Precision SMT Placement: Automated high-speed lines supporting 01005 passives, 0.35mm pitch micro-BGAs, Package-on-Package (PoP), and nitrogen-purged 10-zone reflow soldering.
•Advanced In-Line Verification: 100% 3D Solder Paste Inspection (SPI), multi-angle 3D AOI, high-resolution 3D Automated X-Ray (AXI), flying probe testing, and custom bed-of-nails ICT fixture fabrication.
•Free Engineering DFM & DFA Reviews: Every project receives a comprehensive pre-production Design for Manufacturability (DFM) and Design for Assembly (DFA) audit to eliminate footprint discrepancies, resolve MSL handling, and optimize reflow thermal mass before line setup.
Ready to manufacture your electronic assembly with guaranteed quality and transparent factory pricing? Upload your Gerber, BOM, and Centroid data for an instant quotation, or contact our engineering team today for a complete PCBA specification and DFM review.
{{ commentCount }} Comments